Solutions for Excessive Burr in Slitting Line Optimization of Slitting‑Blade Clearance
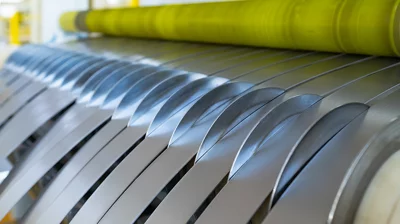
Large burrs on slit strip edges cause cutting hazards, assembly defects and die damage in subsequent stamping
Dive into our Product Knowledge Hub, where our expert sales team shares valuable insights on product knowledge and after-sales service, and more. Gain exclusive access to insider tips and resources to enhance your product ownership experience.
Large burrs on slit strip edges cause cutting hazards, assembly defects and die damage in subsequent stamping
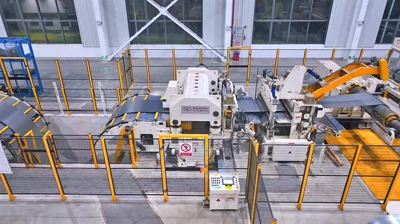
Core parameters for slitting‑line selection are coil width, number of slits and target strip width. Improper m
Cut‑to‑length lines integrate uncoiling, leveling and fixed‑length cross‑cutting to convert metal coils into f
Multi‑specification small‑batch production features frequent product change‑overs, where change‑over duration
Stamping‑shop automation starts from the fundamental feeding process. Conventional manual feeding is slow, low
Proper installation and commissioning are critical for stable operation of 3‑in‑1 feeders. Poor installation m
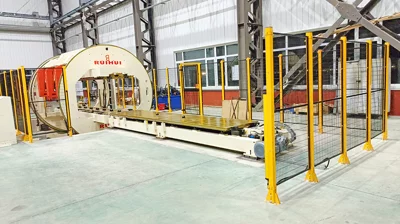
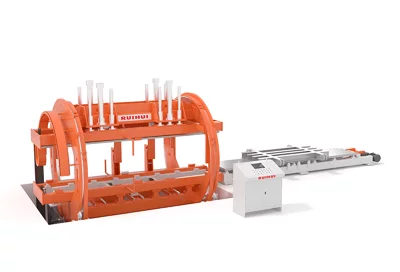
Upenders flip sheet‑metal stacks by 90° or 180° in stamping workshops. Its control system manages parameters s
Upenders in stamping workshops flip sheet stacks by 90° or 180°. Excessively low rotation speed causes line bo
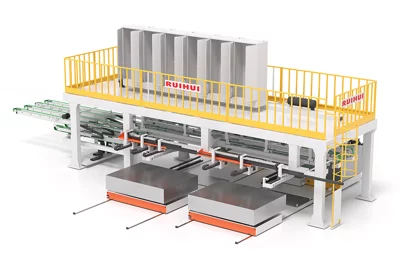
Stackers are installed at the outlet of cut‑to‑length lines for sheet stacking. Conventional manual trolley re
Traditional cut‑to‑length lines rely on manual stacking at line‑end, which is labor‑intensive and yields untid