

Cycle‑Time Improvement for Hot‑Stamping Lines Rapid‑Transfer Methods for High‑Temperature Blanks
Share to : 


The cycle‑time performance of hot‑stamping lines differs from conventional stamping lines. Slow cycle‑time not only reduces output but also causes quality defects. Blanks keep cooling after exiting the furnace; excessive transfer time leads to insufficient blank temperature and substandard part strength. Therefore, improving line takt essentially relies on rapid transfer of high‑temperature blanks.
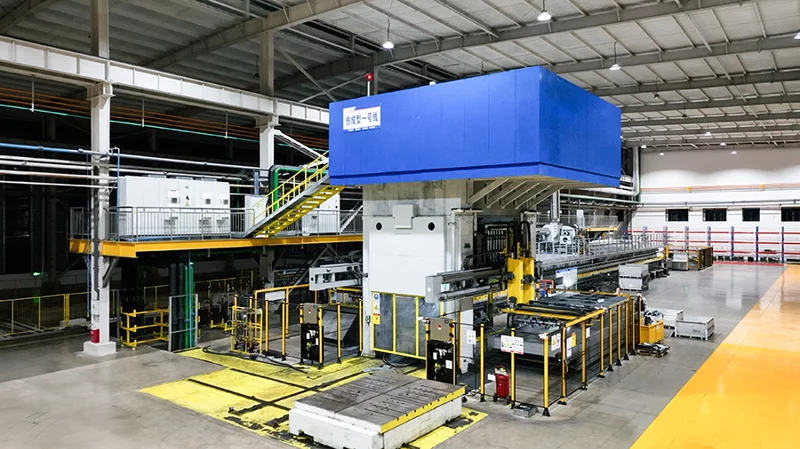
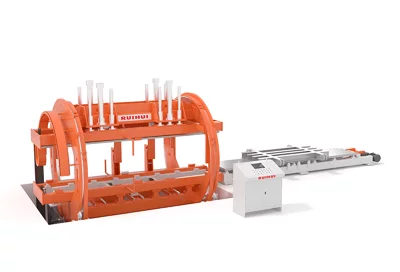
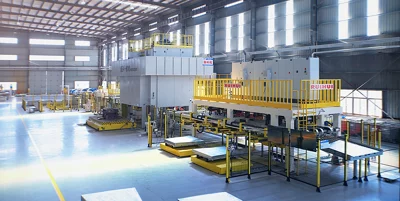
The production loop includes furnace heating, blank discharging, robot picking, material feeding, stamping‑quenching and part unloading. Heating duration is fixed, so optimization focuses on shortening the transfer interval from furnace discharge to die stamping. Shorter transfer time preserves blank temperature and raises overall takt.
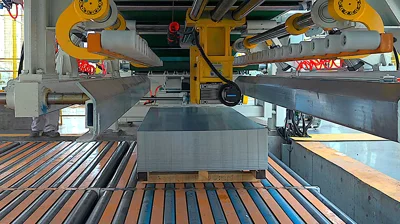
Servo‑driven manipulators with excellent acceleration‑deceleration characteristics deliver swift pick‑and‑place movements. Optimized motion trajectories shorten travel paths and eliminate redundant motions to cut transfer duration.
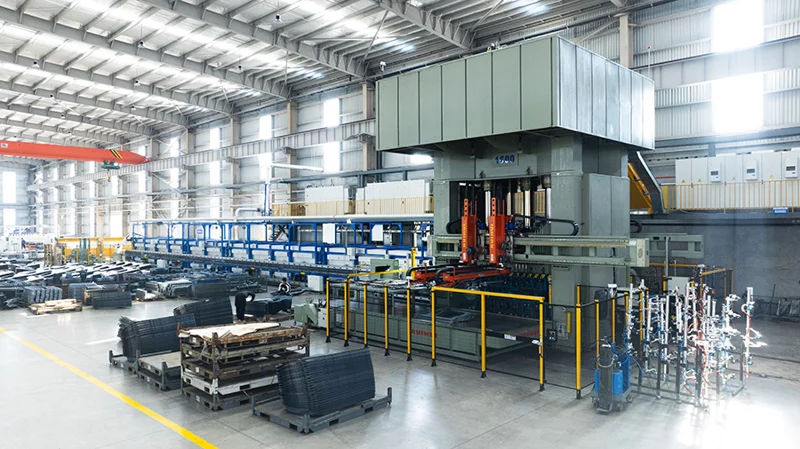
Tight sequential coordination among furnace discharging, manipulator picking and press stamping is required. The press shall start stamping immediately once the manipulator finishes part placement and fully retracts. Well‑designed signal interaction and timing logic eliminate idle waiting between processes and compress total cycle time.
Furnace discharging rhythm must match manipulator handling capacity. Premature discharge causes heat loss while blanks wait at the furnace outlet; delayed discharge results in idle time for manipulators and presses. Proper rhythm matching ensures smooth line operation.
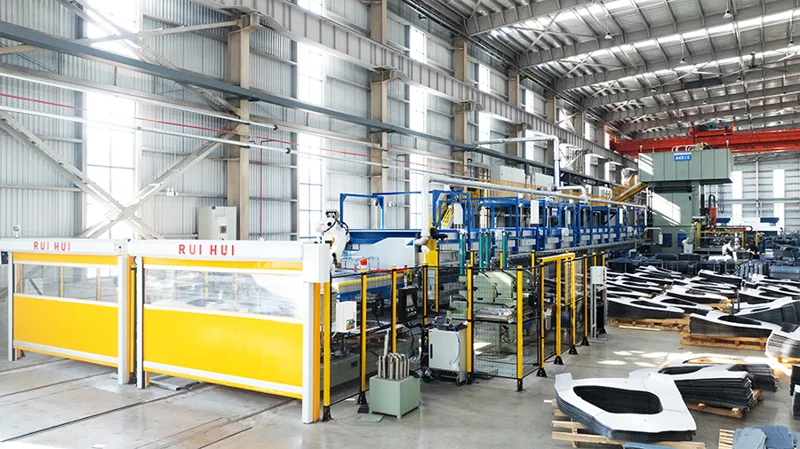
Thermal‑retention measures can be adopted to mitigate heat loss during transfer. Valid takt improvement shall guarantee stable stamping quality alongside higher throughput.
Heat‑resistant alloy grippers serve as the foundation for reliable high‑speed transfer. The end‑of‑arm tools withstand high ambient temperature by material properties to sustain long‑term stable operation.
To sum up, higher hot‑stamping‑line takt is achieved by fast blank discharging, rapid transfer and prompt die feeding. Optimized manipulator motion, tight process coupling and matched furnace discharging rhythm shorten transfer time, preserving blank temperature and improving both production capacity and component quality.
Guangdong Ruihui Intelligent Technology Co., Ltd., a national Specialized, Refined, Differential and Innovative “Little Giant” enterprise headquartered in Dongguan with over 20‑year stamping‑automation experience, employs more than 400 staff including over 80 R&D engineers. For hot‑stamping‑line cycle‑time optimization, Ruihui focuses on shortening high‑temperature‑blank transfer time via servo‑driven manipulators, optimized motion trajectories and compact timing sequences. Heat‑resistant alloy grippers ensure stable transfer performance. The company has supplied hot‑stamping lines for multiple automotive‑component manufacturers. Nearly 5,000 sets of Ruihui‑manufactured equipment operate globally, with cooperation cases covering well‑known OEMs and Tier‑one suppliers such as BYD, Geely, Volkswagen, Tesla, BMW, Mercedes‑Benz, Honda and Jaguar Land Rover.
With years of hands-on experience, I have honed my skills in navigating the complexities of global commerce, offering invaluable insights and solutions to address customer needs. My commitment to excellence and dedication to customer satisfaction ensure that I deliver exceptional service, guiding clients through every step of the trading process with confidence and proficiency.
You may also like
Related News
Latest Update