

How to Plan a Hot‑Forming Stamping Line Configuration Scheme for Furnaces Presses and Manipulators
Share to : 


Hot‑forming stamping is a process for manufacturing high‑strength steel components. Sheet blanks are heated to 800‑900 °C, stamped while hot, and rapidly quenched inside dies to produce high‑strength and lightweight parts. A functional hot‑forming line relies on three core units: heating furnace, press and manipulator. Key planning and configuration points are outlined below.
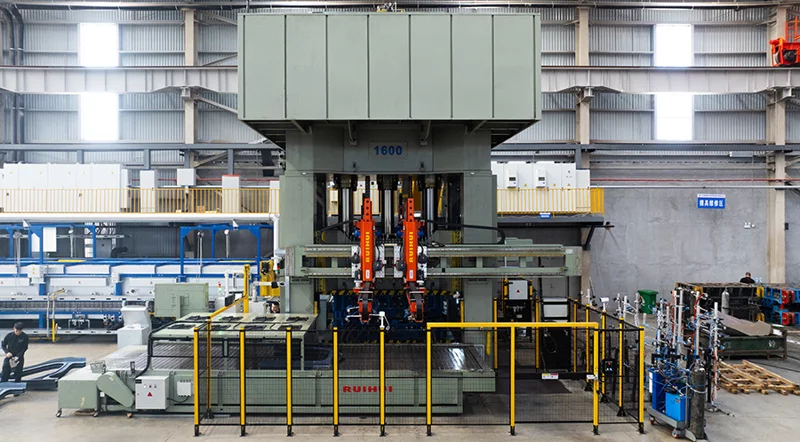
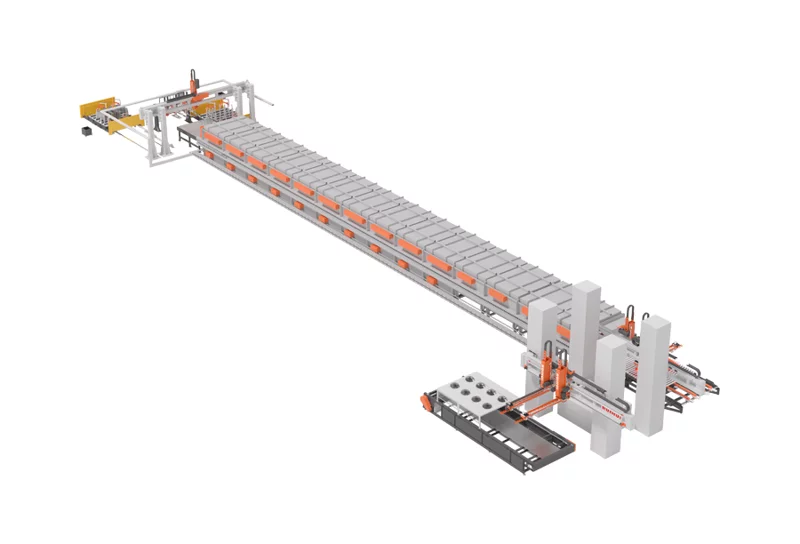
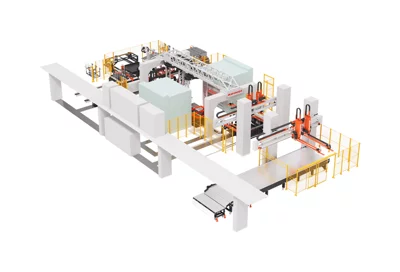
First, clarify the overall workflow. Sheets are loaded and fed into the heating furnace to reach 800‑900 °C. Hot blanks are then extracted from the furnace outlet and transferred into the press die for hot stamping. Forming and rapid quenching take place simultaneously within dies, after which finished parts are discharged for subsequent processes. The critical link is “furnace discharge‑material feeding‑stamping”. Temperature drops rapidly once blanks leave the furnace. Blanks must be delivered into dies within a limited time window; delayed feeding leads to insufficient quenching and failure to meet target part strength. Coordination among heating furnace, manipulator and press constitutes the core of line planning.
For heating‑furnace configuration, furnace selection depends on sheet dimensions, thickness and output requirements. Sufficient heating capacity ensures uniform and stable blank temperature to guarantee stamping quality. Furnace feeding and discharging modes shall match manipulator picking motions. The position and discharge rhythm of the furnace outlet must be defined in the planning phase.
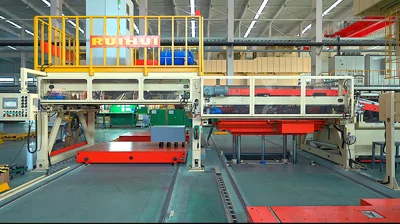
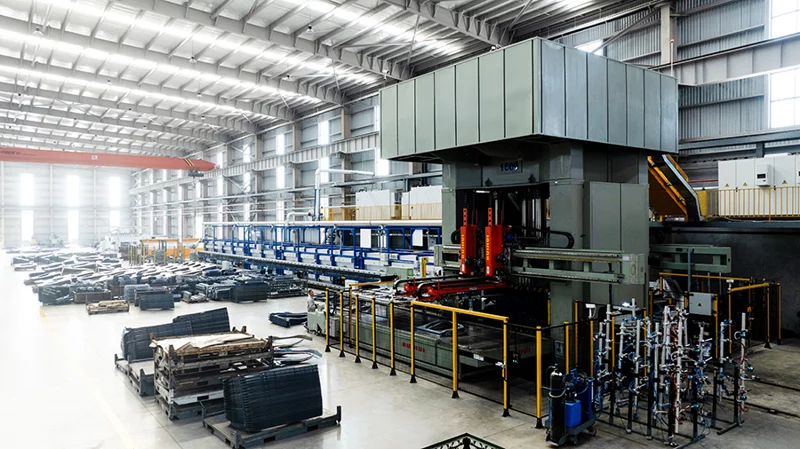
As for manipulator configuration, hot‑forming loading‑unloading manipulators perform two main tasks: extracting red‑hot blanks from the furnace and delivering them to the press, and removing stamped finished parts from dies for downstream handling. Manipulators must adapt to high‑temperature operating conditions. End‑effectors directly contacting 800‑900 °C blanks adopt high‑temperature‑resistant alloy grippers that resist deformation and failure under prolonged heat exposure. Manipulator stroke shall cover the distance between furnace outlet and press, payload shall support blank and part weight, and high‑speed accurate motion is required to meet cycle‑time constraints after blank discharge.
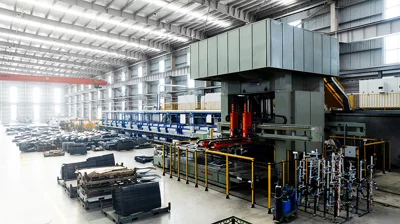
Regarding press configuration, hot‑forming presses must deliver adequate stamping force and support rapid in‑die cooling. Press takt shall synchronize with furnace discharge rhythm and manipulator pick‑and‑feed speed to enable continuous line operation.
Consider upstream and downstream auxiliary equipment. The upstream feeding system transports cold blanks to the furnace inlet for automated loading to reduce manual intervention. Downstream equipment handles collection and transfer of stamped parts via conveyors and stacking devices to complete the full production setup.
Several critical points should be emphasized during planning. First, precise signal interaction and time‑sequence coordination among furnace discharging, manipulator picking and press stamping are required; delay in any unit will disrupt the whole line. Second, comprehensive safety protection for high‑temperature environments is mandatory, and safety interlocks between manipulators and presses are non‑negotiable. Third, minimize heat loss by shortening the interval between blank discharge and stamping through fast manipulator movements and optimized line timing. Fourth, ensure good maintainability. High‑temperature conditions accelerate component wear, so end‑effectors and heat‑insulated parts of manipulators shall be easy to inspect and replace.
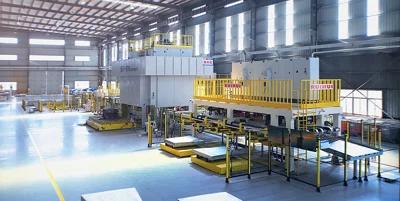
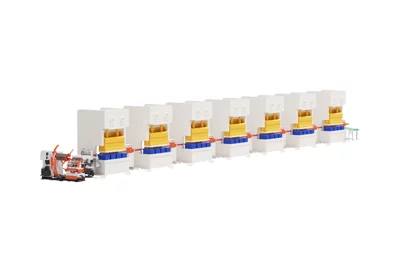
Essentially, hot‑forming stamping‑line planning integrates heating furnace, press and manipulator into a rhythm‑aligned production system. Seamless process links from blank feeding‑in‑furnace to finished‑part output enable efficient and stable line performance.
Guangdong Ruihui Intelligent Technology Co., Ltd. has more than 20‑year experience in stamping automation and is a national Specialized, Refined, Differential and Innovative “Little Giant” enterprise. Headquartered in Dongguan, it has over 400 employees including more than 80 R&D engineers. Ruihui provides complete automated solutions for hot‑forming stamping lines covering furnace feeding/discharging, high‑temperature loading‑unloading manipulators and press timing coordination for whole‑line integration. Purpose‑built manipulators adopt high‑temperature‑resistant alloy grippers together with thermal‑insulation protection for long‑term stable high‑temperature operation, with mature timing coordination and safety interlock functions. Ruihui has delivered multiple hot‑forming automated lines for automotive‑component manufacturers. Nearly 5,000 sets of Ruihui‑manufactured equipment operate at home and overseas, serving well‑known OEMs and Tier‑one suppliers such as BYD, Geely, Volkswagen, Tesla, BMW, Mercedes‑Benz, Honda and Jaguar Land Rover, with extensive practical experience in hot‑forming applications.
With years of hands-on experience, I have honed my skills in navigating the complexities of global commerce, offering invaluable insights and solutions to address customer needs. My commitment to excellence and dedication to customer satisfaction ensure that I deliver exceptional service, guiding clients through every step of the trading process with confidence and proficiency.
Related Topics:
hot stampingYou may also like
Related News
Latest Update